
mong various chemical materials, specialty rubber has become a key product widely used across transportation, defense, industrial manufacturing, agriculture, and consumer goods. As production capacity expands, manufacturers are increasingly facing challenges in managing complex warehousing and logistics operations.
Storage Challenges in Specialty Rubber Warehousing
Unlike many standard industrial products, specialty rubber materials present unique storage requirements due to their diverse chemical properties and sensitivity to environmental conditions.
Common operational challenges include:
1. Complex Product Variants
Specialty rubber often includes numerous product types, formulations, and packaging formats. Traditional warehouses typically rely on floor stacking or static racking layouts, which makes it difficult to implement structured inventory management or FIFO (First-In-First-Out) control.
Without systematic storage management, products may experience aging, prolonged storage cycles, or inefficient retrieval processes.
2. Limited Visibility of Inventory
Manual warehouse operations often depend on periodic inventory counting and paper-based records. This can lead to inconsistencies between physical stock and system records, affecting production planning and supply chain coordination.
3. Disconnected Production and Logistics Processes
In many factories, warehouse operations are not fully integrated with production planning systems. As a result, material movements require extensive manual handling, increasing labor costs and reducing operational efficiency.

Automation as a Key Enabler
Modern automated warehouse technologies are increasingly being adopted to address these challenges.
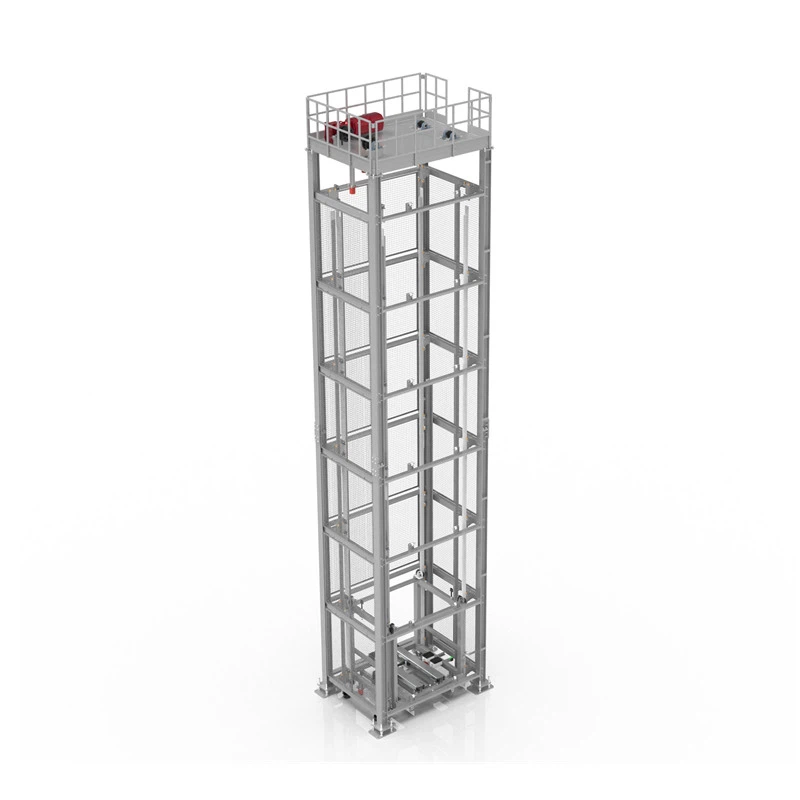
Automated Storage and Retrieval Systems (AS/RS) utilize high-bay racking structures combined with intelligent handling equipment, enabling vertical storage and significantly improving space utilization within the same facility footprint.
Automated systems may include:
● Stacker cranes
● Four-way shuttle robots
● Rail-guided vehicles (RGV)
● Conveyor systems
● Intelligent warehouse software platforms such as WMS and WCS
Together, these systems enable automated inbound, storage, and outbound operations.
In addition to improving operational efficiency, automated warehouses can help manufacturers maintain more structured inventory control and support FIFO inventory management strategies.

Supporting the Next Phase of Chemical Industry Development
As chemical manufacturers continue to expand production capacity and introduce more diversified product portfolios, the role of automated intralogistics systems will become increasingly important.
By integrating warehouse automation with enterprise systems such as ERP and MES, companies can build more coordinated production and logistics workflows. This integration enables better visibility of inventory data and supports more accurate planning decisions.
Warehouse automation therefore plays an essential role in helping chemical material manufacturers improve operational efficiency while supporting the broader transition toward digitalized and intelligent manufacturing environments.