Introduction to Chain Conveyor
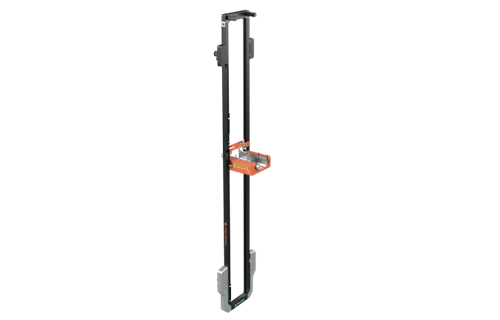
A chain conveyor is a type of conveyor system that uses chains to move materials from one place to another. It consists of a chain, which is usually made of metal links, and a series of sprockets that guide and drive the chain. Chain conveyors are widely used in various industries such as manufacturing, mining, food processing, and logistics. They are known for their durability, high load - carrying capacity, and ability to operate in harsh environments. Chain conveyors can handle a wide range of materials, including heavy and bulky items, and can be customized to meet specific application requirements.
10 Leading Chain Conveyor Factories
1. DELIECN
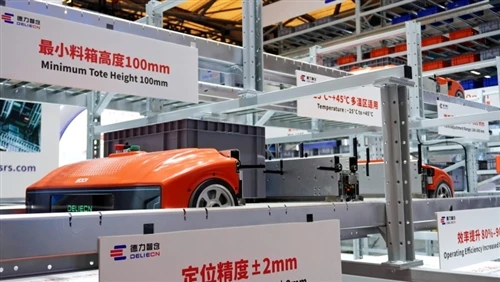
Company IntroductionDELIECN is a well - established company in the field of chain conveyors. It has been dedicated to the research, development, production, and sales of chain conveyor systems for many years. The company is committed to providing high - quality products and excellent customer service. DELIECN's R & D team is constantly innovating to improve the performance and efficiency of its chain conveyors. They use advanced manufacturing technologies and high - quality materials to ensure the reliability and durability of their products.
Features in Chain Conveyor
- Customization: DELIECN offers a high degree of customization. They can design chain conveyors according to the specific needs of different industries, such as the size, shape, and weight of the materials to be conveyed, as well as the layout of the production line.
- High - speed operation: Their chain conveyors are capable of high - speed operation, which can significantly improve the production efficiency. This is especially important for industries with high - volume production requirements.
- Low maintenance: DELIECN's chain conveyors are designed with low - maintenance features. The use of high - quality components and advanced lubrication systems reduces the frequency of maintenance and extends the service life of the equipment.
Advantages
- Technical expertise: The company has a team of experienced engineers and technicians who have in - depth knowledge of chain conveyor technology. They can provide professional technical support and solutions to customers.
- Quality control: DELIECN has a strict quality control system. Every chain conveyor undergoes multiple inspections during the production process to ensure that it meets the highest quality standards.
- Customer - centric service: The company focuses on customer satisfaction. They provide comprehensive pre - sales and after - sales services, including installation, commissioning, and maintenance training.
Website: https://www.deliecn.com/

2. Demag Cranes & Components GmbH
Company IntroductionDemag Cranes & Components GmbH is a globally recognized company with a long - standing history in the material handling industry. It was founded in 1819 and has since grown into a leading provider of innovative lifting and conveying solutions. The company has a wide range of products, including chain conveyors, which are used in various industrial applications. Demag's chain conveyors are known for their precision engineering and high - quality construction.
Features in Chain Conveyor
- Modular design: Demag's chain conveyors are based on a modular design concept. This allows for easy installation, expansion, and modification of the conveyor system. Different modules can be combined to meet the specific requirements of different production processes.
- High - precision movement: The company uses advanced control systems to ensure high - precision movement of the chain conveyor. This is crucial for applications where accurate positioning of materials is required, such as in assembly lines.
- Energy - efficient: Demag is committed to developing energy - efficient products. Their chain conveyors are designed to minimize energy consumption while maintaining high performance.
Advantages
- Global presence: Demag has a global network of sales and service centers, which enables it to provide prompt and efficient support to customers around the world.
- Innovation: The company invests heavily in research and development to continuously improve its products. It is at the forefront of technological advancements in the chain conveyor industry.
- Safety features: Demag's chain conveyors are equipped with a variety of safety features, such as overload protection, emergency stop buttons, and safety guards, to ensure the safety of operators and the smooth operation of the equipment.
3. Rexnord Industries LLC
Company IntroductionRexnord Industries LLC is a leading manufacturer of power transmission and conveyor products. With a history dating back over 100 years, the company has a wealth of experience in the industry. Rexnord offers a comprehensive range of chain conveyors that are suitable for a wide variety of applications, from light - duty to heavy - duty.
Features in Chain Conveyor
- Robust construction: Rexnord's chain conveyors are built with high - strength materials, making them capable of withstanding heavy loads and harsh operating conditions. The chains are designed to be wear - resistant and have a long service life.
- Versatile applications: The company's chain conveyors can be used in many industries, including automotive, food and beverage, and mining. They can handle different types of materials, such as bulk solids, packaged goods, and heavy components.
- Advanced chain technology: Rexnord uses advanced chain manufacturing technology to improve the performance of its conveyors. Their chains have excellent tensile strength and flexibility, which allows for smooth and efficient operation.
Advantages
- Extensive product portfolio: Rexnord offers a wide range of chain conveyor products, which gives customers more options to choose from according to their specific needs.
- Technical support: The company provides comprehensive technical support to its customers. Their team of experts can assist with installation, maintenance, and troubleshooting of the chain conveyors.
- Industry reputation: Rexnord has a good reputation in the industry for its high - quality products and reliable service. It is trusted by many customers around the world.
4. Intralox
Company IntroductionIntralox is a pioneer in the development of modular plastic belt and chain conveyor systems. The company was founded in 1972 and has since become a global leader in the field. Intralox focuses on providing innovative solutions for material handling, with a particular emphasis on food processing, packaging, and distribution industries.
Features in Chain Conveyor
- Sanitary design: Intralox's chain conveyors are designed with a focus on hygiene, which is especially important in the food processing industry. The modular plastic belts are easy to clean and resistant to bacteria and other contaminants.
- Flexible configuration: The company offers a wide range of conveyor configurations, including straight, curved, and inclined conveyors. This allows for the creation of complex conveyor systems to meet the specific layout requirements of different production facilities.
- Energy - saving: Intralox's chain conveyors are designed to be energy - efficient. The low - friction design of the modular plastic belts reduces the power consumption of the conveyor system.
Advantages
- Innovation in materials: Intralox is constantly developing new materials for its chain conveyors. The use of advanced plastics and polymers improves the performance and durability of the conveyors.
- Global service network: The company has a global service network that can provide quick response and support to customers. This ensures the smooth operation of the conveyor systems.
- Environmental friendliness: Intralox is committed to environmental protection. Its products are designed to be recyclable and have a low environmental impact.
5. Dorner Mfg. Corp.
Company IntroductionDorner Mfg. Corp. is a leading manufacturer of conveyor systems, including chain conveyors. The company was founded in 1973 and has a strong reputation for providing high - quality, reliable, and innovative conveyor solutions. Dorner's chain conveyors are used in a variety of industries, such as electronics, medical, and automotive.
Features in Chain Conveyor
- Compact design: Dorner's chain conveyors are designed to be compact, which is suitable for applications where space is limited. They can be easily integrated into existing production lines.
- High - speed performance: The company's chain conveyors are capable of high - speed operation, which can improve the production efficiency. They are equipped with advanced drive systems to ensure smooth and stable movement.
- Easy maintenance: Dorner's chain conveyors are designed for easy maintenance. The modular design allows for quick replacement of components, reducing downtime.
Advantages
- Custom engineering: Dorner offers custom - engineered chain conveyor solutions. Their engineering team can work closely with customers to design conveyors that meet their specific requirements.
- Quality assurance: The company has a strict quality assurance system. All products are tested thoroughly before leaving the factory to ensure their performance and reliability.
- Customer service: Dorner provides excellent customer service. They offer training, installation, and after - sales support to ensure that customers can use their chain conveyors effectively.
6. FlexLink Systems AB
Company IntroductionFlexLink Systems AB is a Swedish company that specializes in the design and manufacture of conveyor systems. It has a global presence and is known for its innovative and flexible conveyor solutions. FlexLink's chain conveyors are used in a wide range of industries, including consumer goods, electronics, and pharmaceuticals.
Features in Chain Conveyor
- Flexible layout: FlexLink's chain conveyors can be easily configured to fit different production layouts. They offer a variety of conveyor modules, such as straight, curved, and lifting sections, which can be combined to create a customized conveyor system.
- High - quality components: The company uses high - quality components in its chain conveyors, ensuring their reliability and durability. The chains are designed to have a long service life and can withstand heavy loads.
- Automation integration: FlexLink's chain conveyors can be easily integrated with other automation equipment, such as robots and sorting systems. This allows for the creation of fully automated production lines.
Advantages
- Global support: FlexLink has a global network of sales and service offices, which can provide local support to customers. This ensures that customers can get timely assistance when needed.
- R & D investment: The company invests heavily in research and development to continuously improve its products. It is constantly introducing new technologies and features to its chain conveyors.
- Sustainable solutions: FlexLink is committed to sustainability. Its chain conveyors are designed to be energy - efficient and have a low environmental impact.
7. Interroll Group
Company IntroductionInterroll Group is a leading global provider of material handling solutions, including chain conveyors. The company was founded in 1959 and has a strong presence in the international market. Interroll's chain conveyors are used in various industries, such as logistics, e - commerce, and automotive.
Features in Chain Conveyor
- Smart technology: Interroll's chain conveyors are equipped with smart technology, such as sensors and control systems. This allows for real - time monitoring and optimization of the conveyor operation, improving efficiency and reducing downtime.
- Modular and scalable: The company's chain conveyors are based on a modular design, which makes them easy to install, expand, and modify. They can be scaled up or down according to the changing needs of the production process.
- High - performance drive systems: Interroll uses high - performance drive systems in its chain conveyors, ensuring smooth and efficient operation. The drives are designed to be energy - efficient and have a long service life.
Advantages
- Global market reach: Interroll has a wide global market reach, which enables it to serve customers in different regions. It has a strong brand reputation and is trusted by many large - scale enterprises.
- Innovation leadership: The company is at the forefront of innovation in the material handling industry. It continuously develops new products and technologies to meet the evolving needs of customers.
- Comprehensive service: Interroll provides comprehensive service, including installation, commissioning, maintenance, and spare parts supply. This ensures the long - term reliable operation of its chain conveyors.
8. Bosch Rexroth AG
Company IntroductionBosch Rexroth AG is a well - known company in the field of industrial automation and drive technology. It offers a wide range of products, including chain conveyors. Bosch Rexroth's chain conveyors are used in many industries, such as manufacturing, packaging, and automotive.
Features in Chain Conveyor
- High - precision control: The company uses advanced control technology to achieve high - precision movement of the chain conveyor. This is important for applications where accurate positioning and synchronization are required.
- Robust and reliable: Bosch Rexroth's chain conveyors are built with high - quality materials and components, ensuring their robustness and reliability. They can operate in harsh environments and under heavy loads.
- Integration with automation systems: The chain conveyors can be easily integrated with other automation systems, such as programmable logic controllers (PLCs) and industrial robots. This allows for the creation of fully automated production processes.
Advantages
- Technological strength: Bosch Rexroth has strong technological strength in the field of industrial automation. It can provide advanced solutions for chain conveyor systems, including intelligent control and monitoring.
- Global service network: The company has a global service network, which can provide prompt and efficient support to customers around the world.
- Product quality: Bosch Rexroth is known for its high - quality products. Its chain conveyors are subject to strict quality control during the production process to ensure their performance and reliability.
9. ContiTech Conveyor Belt Group
Company IntroductionContiTech Conveyor Belt Group is a part of the Continental AG, a leading global automotive and industrial supplier. The company specializes in the production of conveyor belts and chain conveyors. ContiTech's chain conveyors are used in a variety of industries, such as mining, cement, and power generation.
Features in Chain Conveyor
- High - strength chains: ContiTech uses high - strength chains in its chain conveyors, which can withstand heavy loads and harsh operating conditions. The chains are designed to have a long service life and high wear resistance.
- Customized solutions: The company offers customized chain conveyor solutions according to the specific requirements of different industries. They can design conveyors with different widths, lengths, and load - carrying capacities.
- Advanced belt technology: In addition to chains, ContiTech also uses advanced belt technology in its chain conveyors. The combination of chains and belts provides a more efficient and reliable conveying solution.
Advantages
- Industry experience: ContiTech has extensive industry experience in the production of conveyor systems. It understands the needs of different industries and can provide appropriate solutions.
- Research and development capabilities: The company invests in research and development to continuously improve its products. It is constantly exploring new materials and technologies to enhance the performance of its chain conveyors.
- Quality management: ContiTech has a strict quality management system. All products are tested and inspected to ensure that they meet the highest quality standards.
10. Fives Group
Company IntroductionFives Group is a global industrial engineering group that offers a wide range of solutions, including chain conveyors. The company has a long history and a strong presence in the international market. Fives' chain conveyors are used in various industries, such as steel, aluminum, and food processing.
Features in Chain Conveyor
- Advanced design: Fives' chain conveyors are designed with advanced engineering concepts. They are optimized for performance, efficiency, and reliability. The conveyors can handle large - scale and complex material handling tasks.
- High - temperature resistance: In industries such as steel and aluminum, high - temperature resistance is crucial. Fives' chain conveyors are designed to operate in high - temperature environments, ensuring the continuous and stable operation of the production process.
- Automation and digitalization: Fives is at the forefront of automation and digitalization in the chain conveyor industry. Their conveyors are equipped with advanced sensors and control systems, which allow for real - time monitoring and optimization of the conveyor operation.
Advantages
- Global project management: Fives has extensive experience in global project management. It can handle large - scale projects from design to installation and commissioning, ensuring the successful implementation of chain conveyor systems.
- Technical innovation: The company is committed to technical innovation. It continuously develops new technologies and solutions to improve the performance and competitiveness of its chain conveyors.
- Customer - focused service: Fives provides customer - focused service. It works closely with customers to understand their needs and provides customized solutions to meet their specific requirements.
Conclusion
The 10 leading chain conveyor factories mentioned above represent the top - level players in the global chain conveyor industry. Each company has its own unique features and advantages, whether it is in terms of product customization, technological innovation, or service quality. DELIECN stands out with its high - degree customization and low - maintenance features. Demag Cranes & Components GmbH is known for its precision engineering and global presence. Rexnord Industries LLC offers a robust and versatile chain conveyor solution. Intralox is a pioneer in modular plastic belt and chain conveyor systems with a focus on hygiene. Dorner Mfg. Corp. provides compact and high - speed chain conveyors. FlexLink Systems AB offers flexible and automated conveyor solutions. Interroll Group is at the forefront of smart technology in chain conveyors. Bosch Rexroth AG combines high - precision control with automation integration. ContiTech Conveyor Belt Group has strong capabilities in high - strength chain and belt technology. Fives Group offers advanced design and high - temperature - resistant chain conveyors.
These companies are driving the development of the chain conveyor industry through continuous innovation and improvement. They are meeting the diverse needs of different industries and contributing to the efficiency and productivity of global manufacturing and logistics operations. As the industry continues to evolve, these leading factories will likely play an even more important role in shaping the future of chain conveyor technology.